 +86 184 3796 0706
 info@destinytrans.com


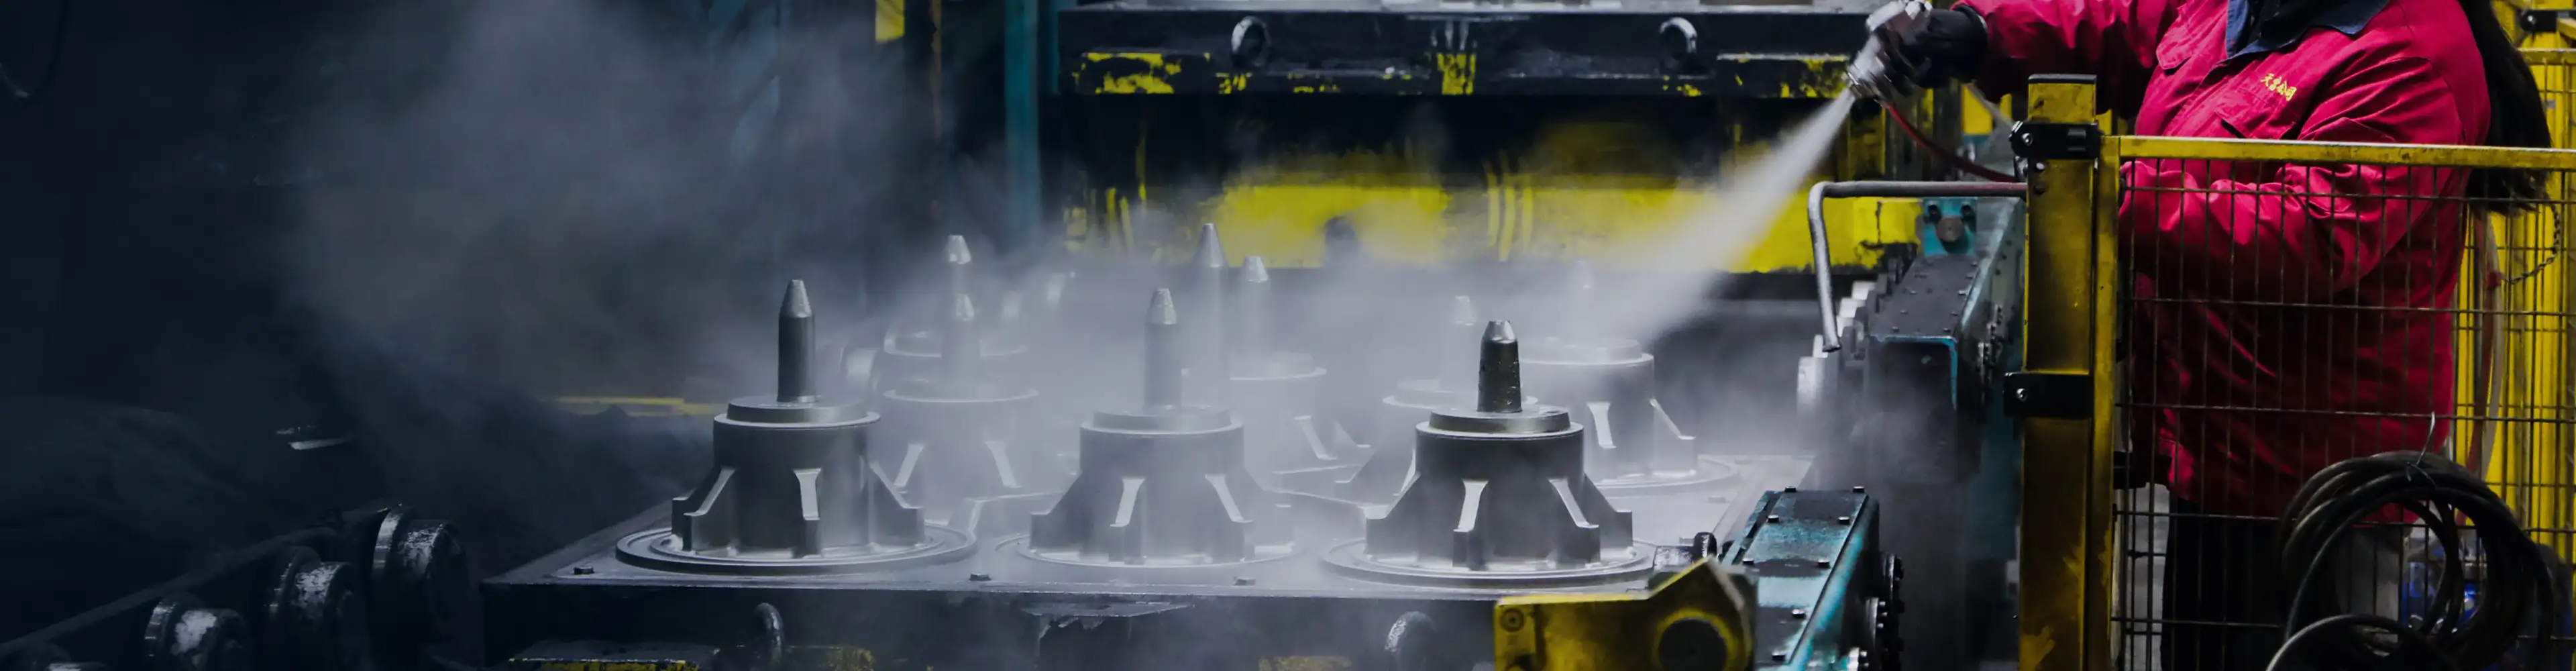
| scope | Specification |
| Core Applications | front axles of heavy trucks and buses |
| Material | cast steel |
| Part Number | 31.GD33G1A2 |
| process | Casting + CNC Precision Machining |
OEM / ODM
Custom from drawings, 3D models, or samples.
Focusing on the design, manufacturing processes, heat treatment techniques, and key quality control points for all types of standard and non-standard gears.
| scope | Specification |
| Core Applications | front axles of heavy trucks and buses |
| Material | cast steel |
| Part Number | 31.GD33G1A2 |
| process | Casting + CNC Precision Machining |
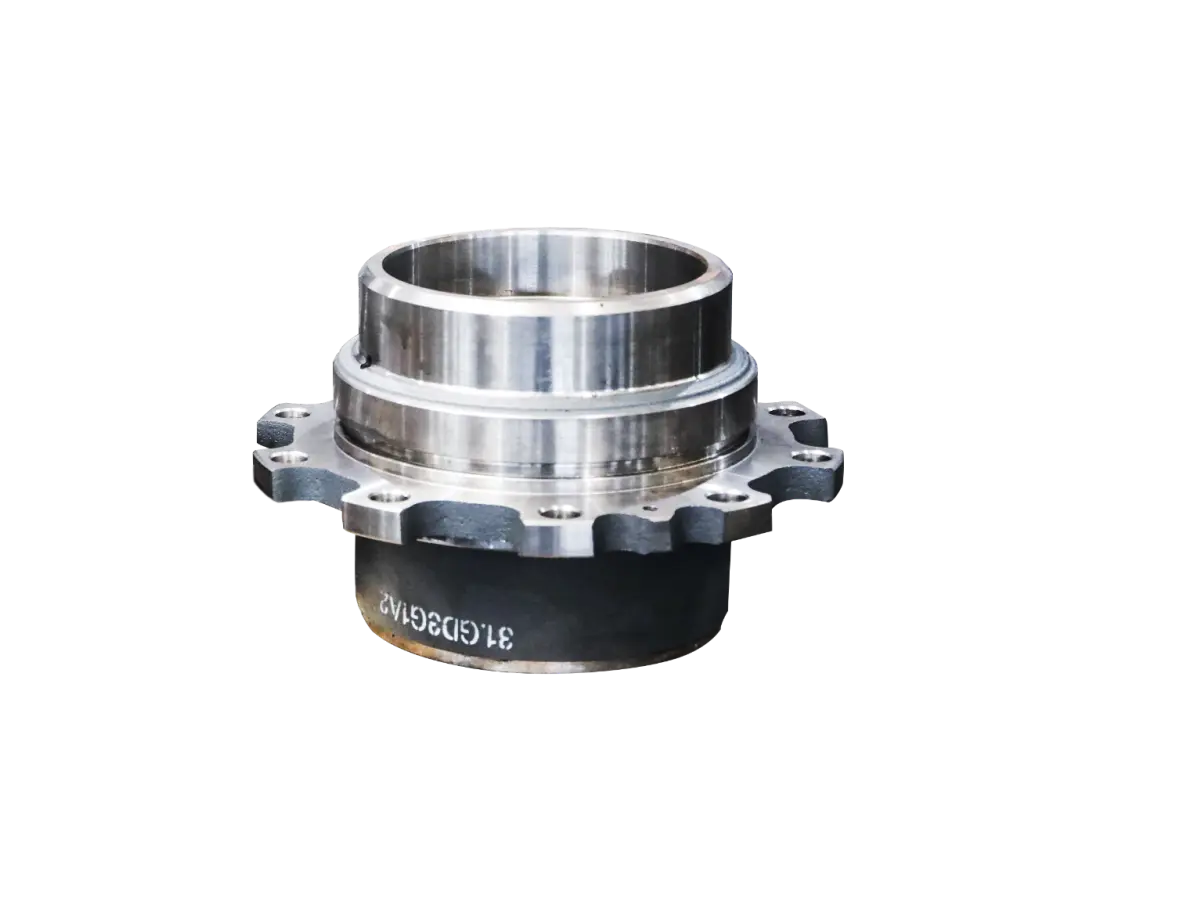
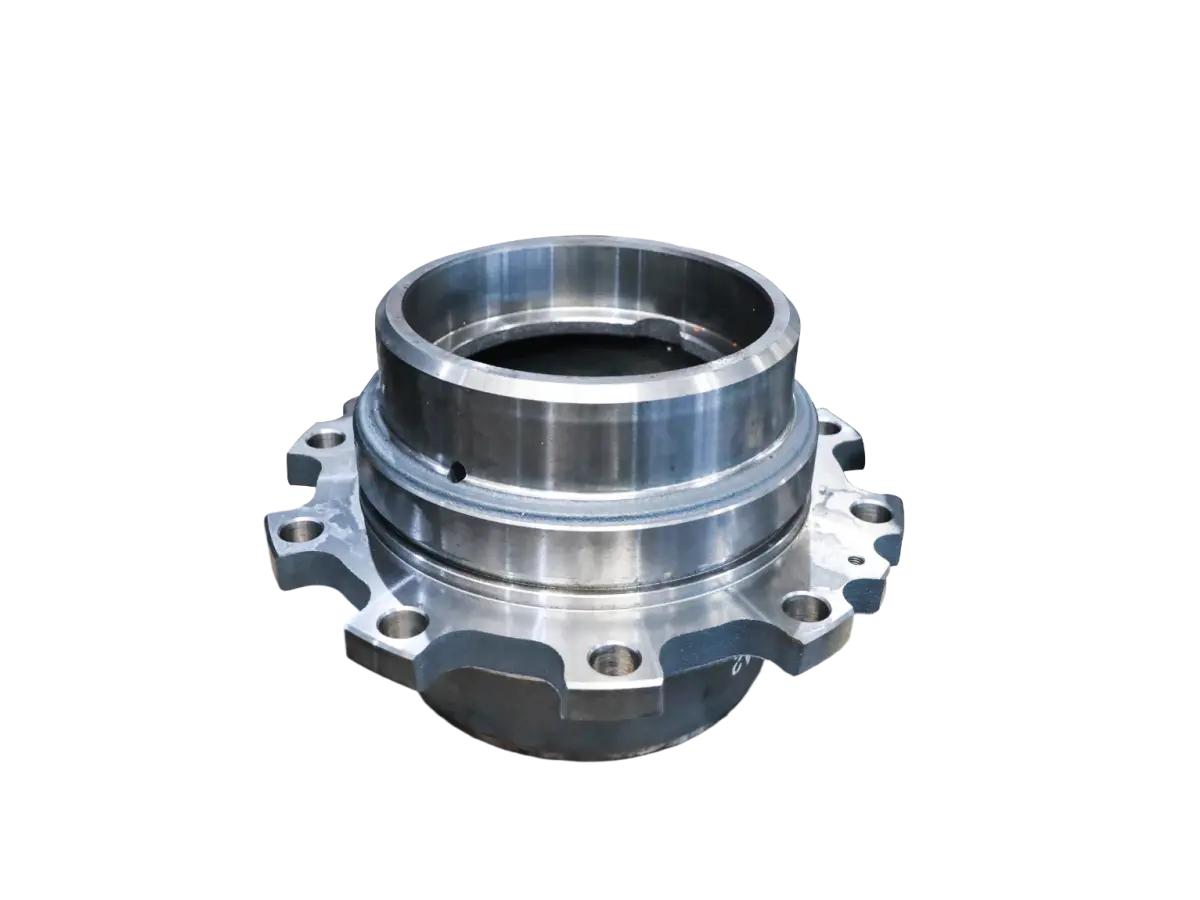
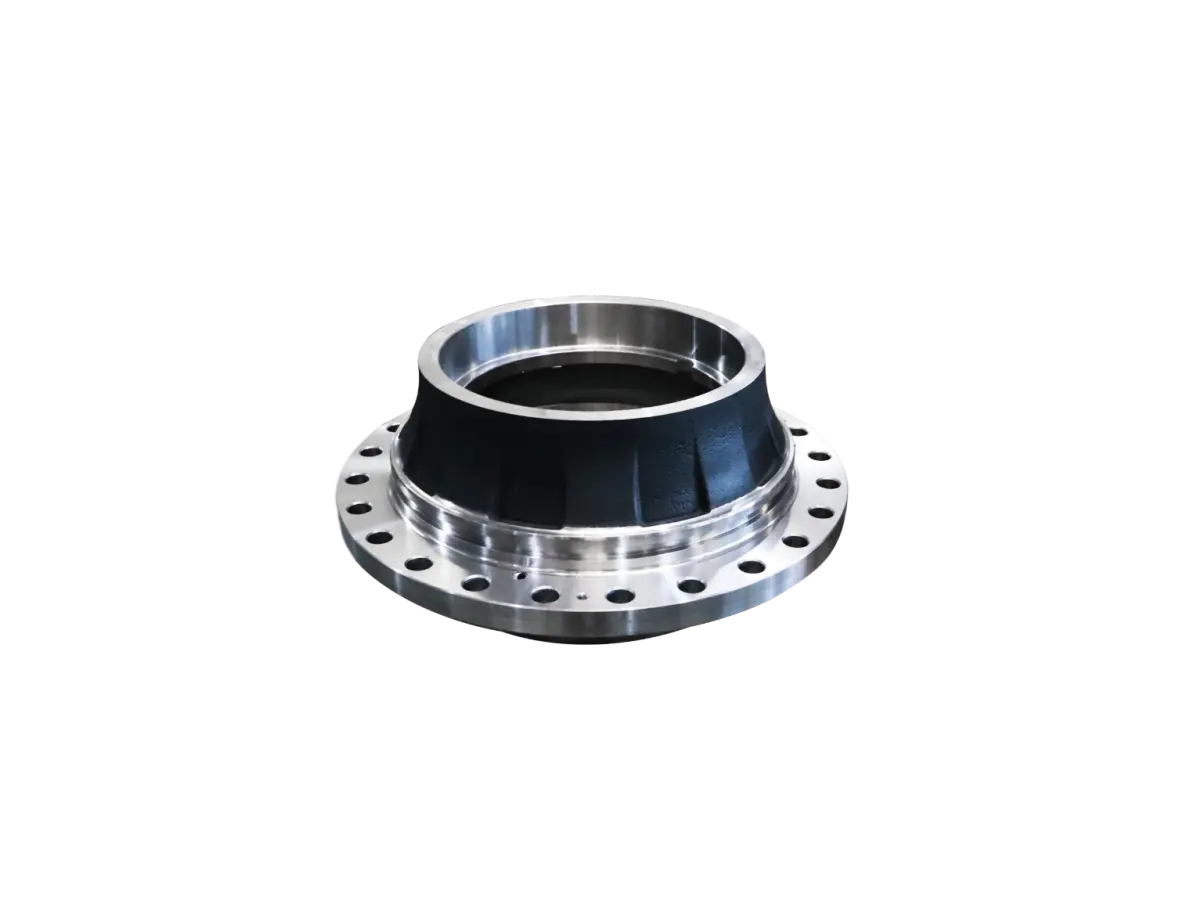
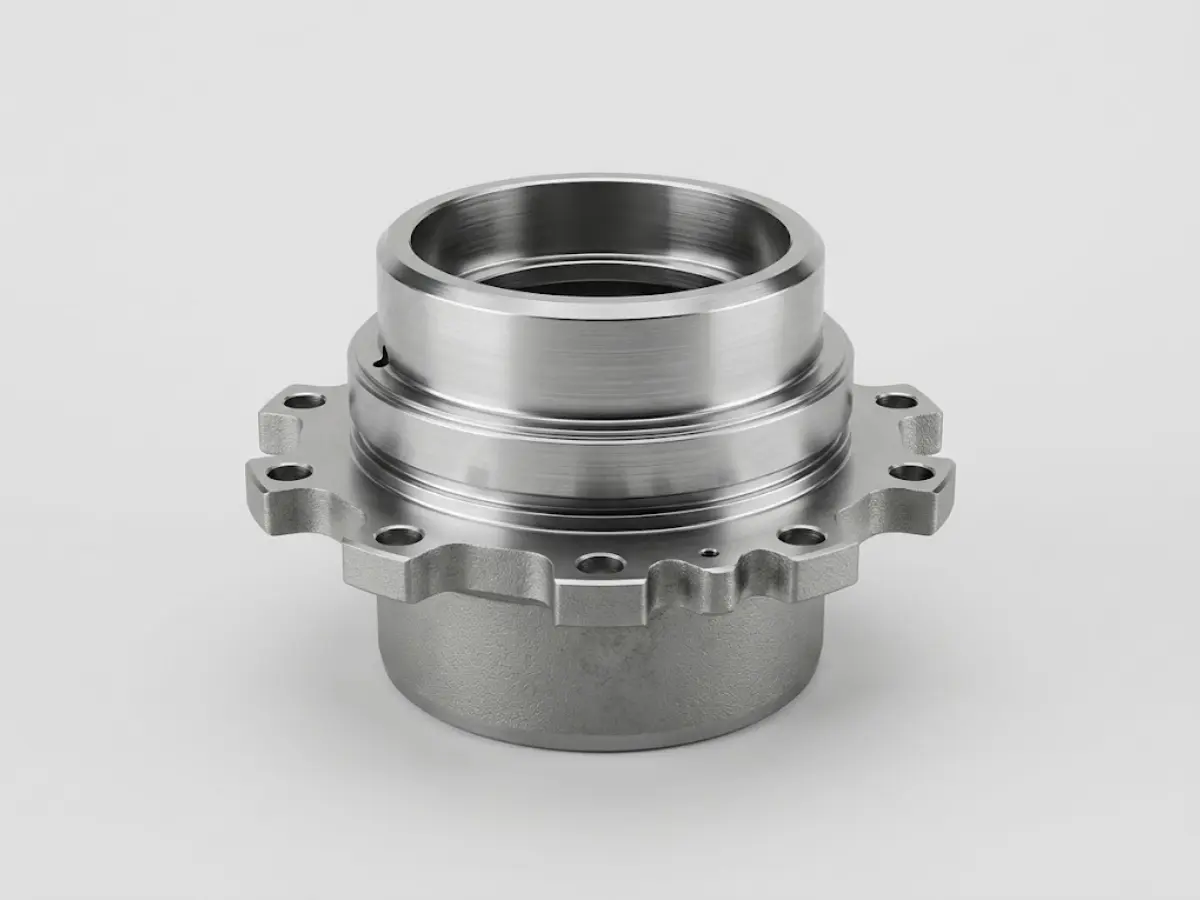
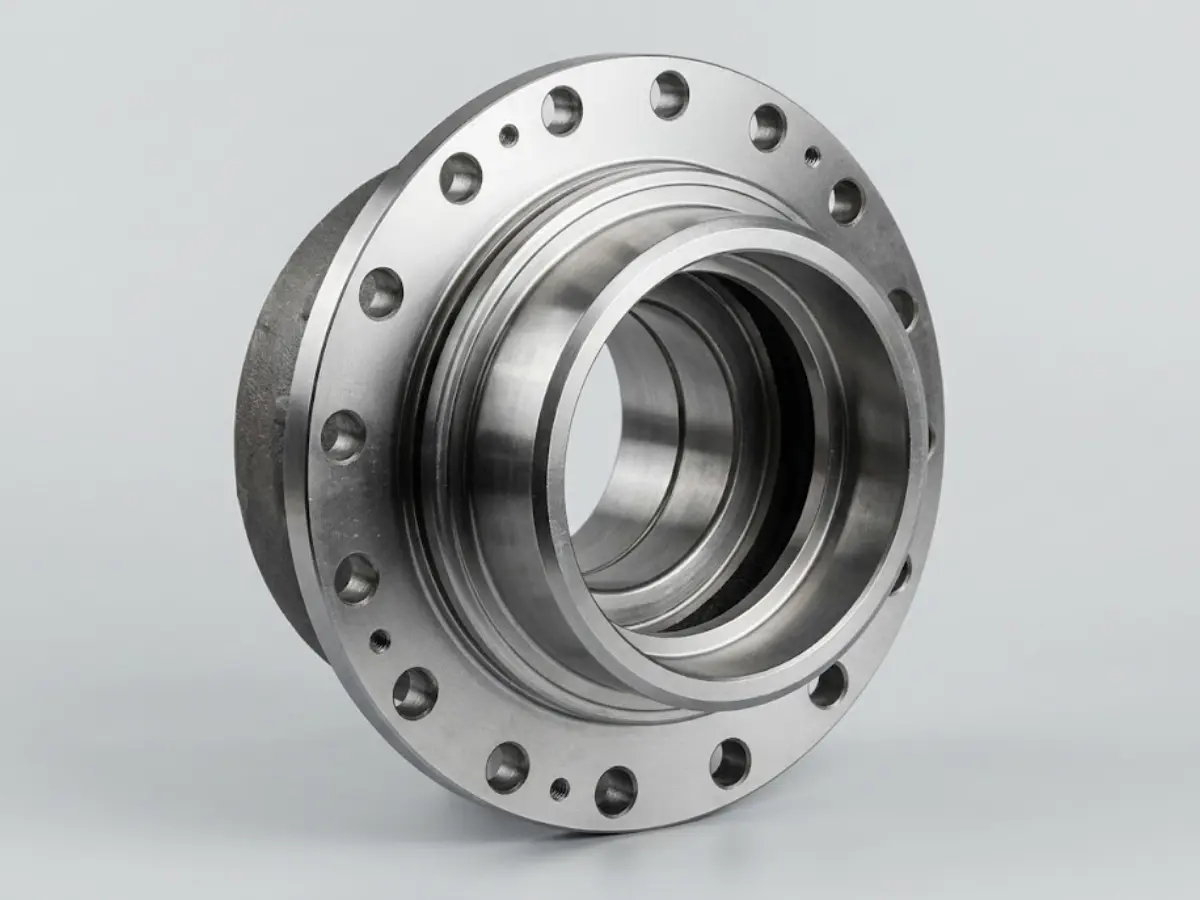
The front wheel hub unit for heavy-duty trucks and buses is a wheel-end structural component installed at the front axle end of heavy-duty trucks, buses, and vans. Made of cast steel and precision-machined using CNC machining, it integrates bearing mounting holes, wheel mounting flanges, and a load-bearing housing for mounting wheel bearings, connecting wheels, and transmitting loads. It is a crucial mechanical connection and load-bearing component in the front wheel-end system of commercial vehicles.
The upper bore is for mounting wheel hub bearings, the middle flange has multiple bolt holes for mounting wheels and related braking components, and the lower housing provides the main structural support. The casting blank is CNC turned, bored, milled, and drilled to form key functional surfaces, combining the structural efficiency of casting with controllable machining accuracy. Part number 31.GD33G1A2 can be used for product identification and matching reference; the final selection should be confirmed based on the target vehicle, axle model, and installation dimensions.
2.1 One-piece casting structure
This product features a one-piece cast structure, consisting of an upper bearing mounting area, a middle hub mounting flange, and a lower load-bearing housing. After casting, key functional surfaces such as bearing holes, flange faces, and bolt holes are precision machined. The integrated structure reduces connection interfaces and provides a stable cast billet for dimensional, positional, and fit control.
Compared to components composed of multiple independent parts, the one-piece cast design reduces connection interfaces and results in a more compact structure. For commercial vehicle front axle applications that bear vehicle loads, braking torque, and road impacts, this one-piece design provides a continuous load transfer path. Actual load-bearing capacity and fatigue performance should be determined based on specific design, material grade, and relevant test results.
2.2 Cast steel materials and CNC precision machining
This component is made of cast steel and is suitable for load-bearing applications at the ends of commercial vehicle wheels. The cast billet is precision-machined using CNC to form bearing holes, flange faces, mounting holes, and other mating surfaces, combining the structural foundation of casting with controllable machining precision. Specific material grades and mechanical properties can be determined based on customer drawings and technical requirements.
Critical machining areas include bearing mounting holes, flange locating surfaces, bolt mounting holes, and other functional mating surfaces. CNC turning, boring, milling, and drilling are employed to control critical dimensions, hole positions, and surface quality in bearing assembly and hub mounting. Applicable tolerances and surface finish requirements should be determined based on relevant drawings and inspection specifications.
2.3 Load-bearing capacity and impact resistance
As a front axle wheel end structural component, the wheel hub unit bears various loads during operation, including vehicle weight, braking and steering forces, and uneven road surfaces. Its flange, housing, and transition area are designed to provide a stable load transfer path, while the cast steel material and precision-machined functional surfaces meet the harsh operating conditions of commercial vehicles.
Bearing bores, flange mounting holes, and mating surfaces are critical functional areas, and their dimensions and machining quality affect the fit between the bearing and hub assembly. Therefore, key dimensions, bore positions, and functional mating surfaces are given special attention during manufacturing. Actual load-bearing capacity, impact performance, and fatigue life should be confirmed based on product design, material specifications, and relevant test results.
This hub unit is specifically designed for the front axle position of heavy-duty trucks, buses, and vans. When selecting a unit, key considerations should be given to bearing bore diameter and fit requirements, the number and pitch circle diameter (PCD) of flange bolt holes, flange mounting dimensions, and the matching dimensions between the housing and the axle spindle. Part number 31.GD33G1A2 can be used as a product identification reference; it is recommended that customers provide the target vehicle, axle model, part number, or drawings before purchasing to confirm compatibility.
This component is suitable for original equipment supply and aftermarket replacement of front axles for commercial vehicles, and its dimensions, material grades, processing requirements, and surface treatments can be customized according to customer drawings. For original equipment or bulk projects, relevant material and dimensional inspection documents and other agreed quality records can be provided according to project requirements.
| scope | Specification |
| Part Number | 31.GD33G1A2 |
| Material | cast steel |
| Manufacturing process | Casting + CNC Precision Machining |
| structure | Upper bearing hole + intermediate wheel mounting flange + lower bearing housing (one-piece) |
| Core features | One-piece cast structure, precision machined functional surfaces |
| Function | Bearing installation + wheel installation + load transfer |
| Apply for position | Front axle spindle end |
| weight | Customization available based on drawings |
| Surface treatment | Rust-proof coating |
| Processing capacity | CNC turning, boring, milling, drilling and finishing of mating surfaces. |
| Testing equipment | Spectrometer, metallographic microscope, hardness tester, coordinate measuring machine, tensile testing machine |
| Delivery documents | Material test report, dimensional inspection report, performance test report, hardness record |
Custom from drawings, 3D models, or samples.
Casting structure evaluation and process design.
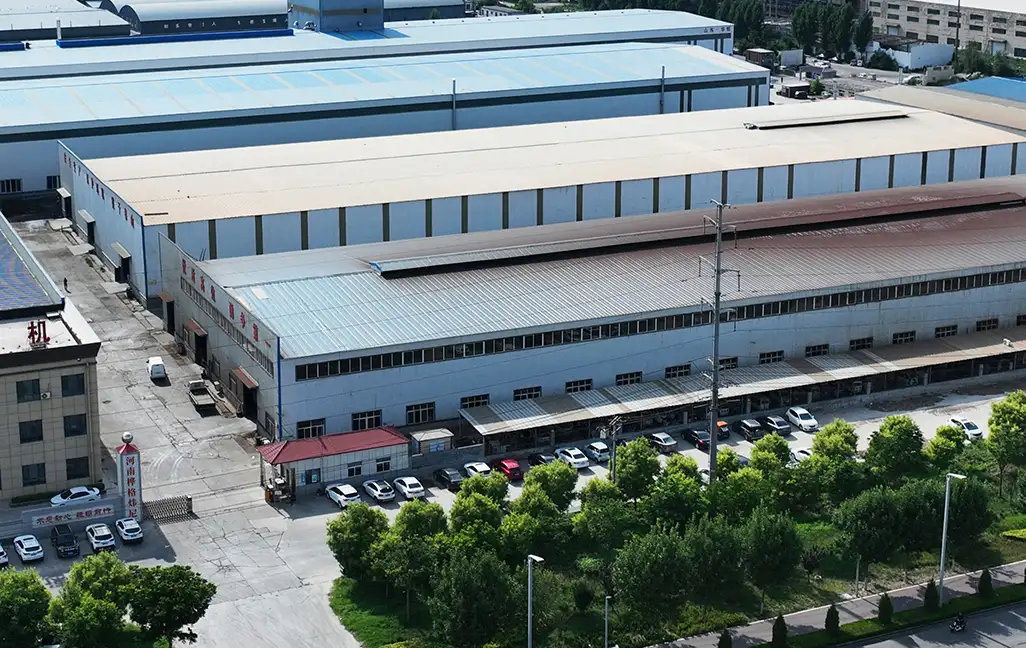
Integrated casting and CNC machining. Annual output: 50,000 tons.
Inspection reports with each delivery.
Scrap steel and iron auto-fed into furnaces, sorted by material grade.
CNC-machined steel/aluminum patterns and sand-pressed foam cores for lost foam process.
Three furnaces alternate for continuous melting with manual and secondary slag removal.
Sand-compacted molds closed and poured; foam cores vaporize as iron fills cavity.
Cooling, de-sanding, grinding, shot blasting, CNC finishing; optional painting and heat treatment.
Spectral, dimensional, mechanical, and load testing; palletized with strapping and film.
In-house casting and CNC machining eliminate coordination overhead between foundry and machine shop, ensuring tighter dimensional control and faster turnaround from pattern to finished part.
Every batch ships with material test reports, dimensional inspection records, and hardness data. Full traceability from incoming material to finished casting with retained samples per batch.
Controlled melting parameters, real-time spectral analysis, and standardized molding procedures ensure consistent mechanical properties and dimensional accuracy across production batches.
Full customization of patterns, text, and reinforcing structures. Exported to 9 countries including Spain, Israel, Jordan, Egypt, Algeria, Malaysia, Thailand, Japan, and Mexico. 7.74M RMB export value in 2023.
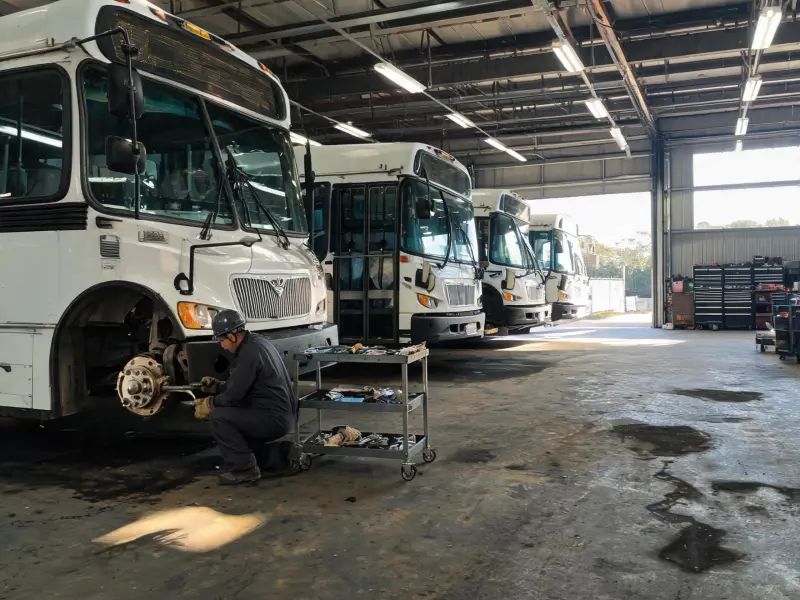
Used for front axle wheel-end maintenance and component replacement on heavy-duty trucks. The hub unit provides the mounting interface for the wheel bearing and wheel assembly and can be matched using the part number, axle model, vehicle information, or relevant installation dimensions.
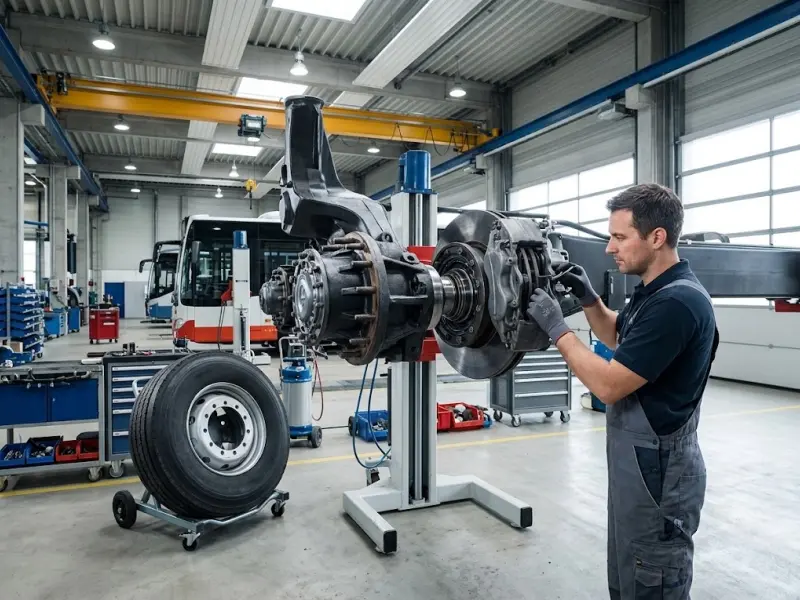
Suitable for city buses and long-distance coaches during front axle inspection, repair, and component replacement. The hub unit is installed at the front axle end and interfaces with the wheel bearing and wheel mounting system. Compatibility should be confirmed according to the vehicle or axle specification.
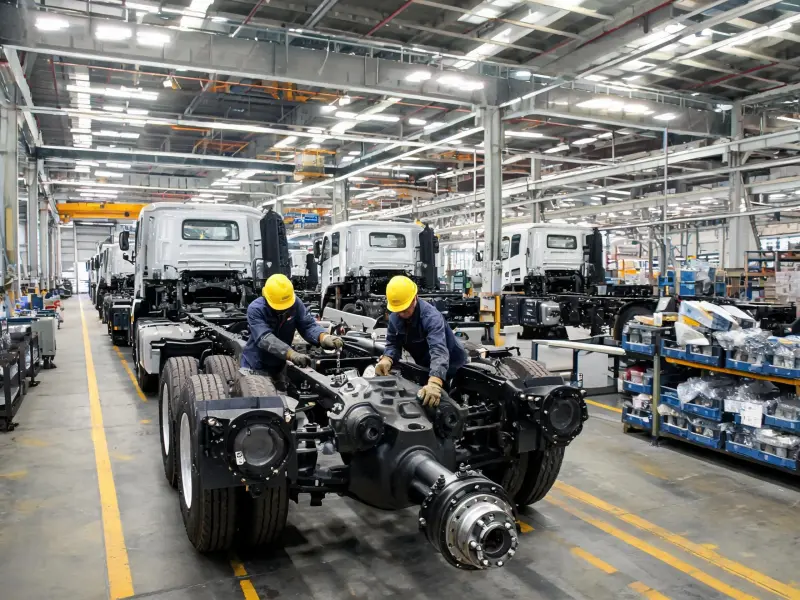
Used in commercial vehicle front axle assembly when the hub unit is installed on the axle spindle and matched with the bearing and wheel mounting components. CNC-machined functional surfaces support consistent dimensional and fit requirements during assembly, subject to the applicable drawing and quality specifications.
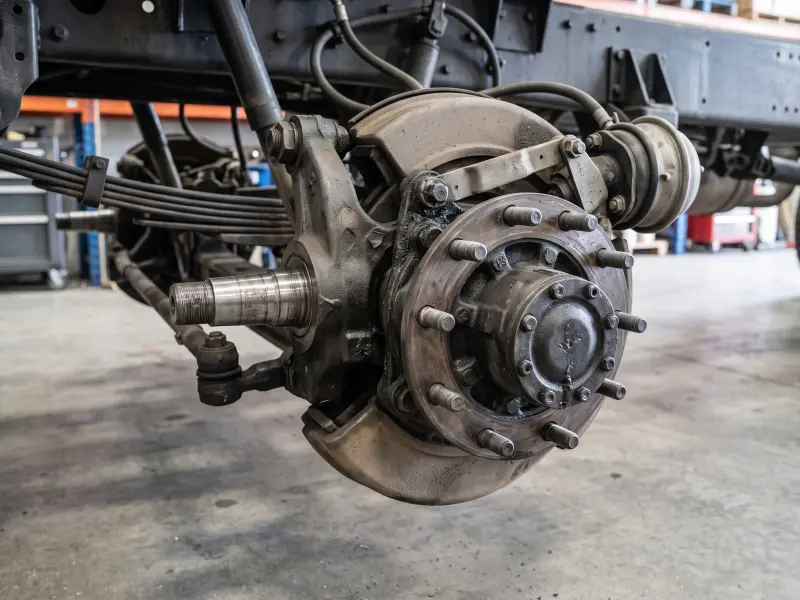
Suitable for aftermarket replacement and spare-parts supply for heavy-duty trucks, buses, and freight vehicles. Customers can use the part number, vehicle or axle information, and installation dimensions to confirm compatibility before ordering, helping reduce the risk of selecting an incorrect replacement component.
Yes. We support OEM/ODM from 2D/3D drawings or physical samples, including material and machining customization.
New samples usually ship in 25-45 days including pattern making, casting, and inspection. Volume schedules are confirmed after process freeze.
Main products include ductile iron manhole covers, grates, textile machine parts, excavator bucket teeth, valve castings, automotive parts, and gear reducer housings, manufactured to GB/T 23858-2009 and GB/T 25628-2010. Materials cover gray iron, ductile iron, and cast steel.
Yes. Equipped with F20 spectrometer, metallographic microscope, hardness tester, universal testing machine, and manhole cover pressure tester. Chemical composition, dimensional, hardness, and material certificates included.
MOQ depends on casting complexity and tooling requirements. Sample orders are accepted. Contact us with your drawings for a specific quotation.
Castings are stacked on wooden pallets with strapping; premium painted products are wrapped with protective film. Packaging is customized to product size and shipping requirements. Quality issues are addressed within 48 hours with repair, replacement, or refund solutions.